
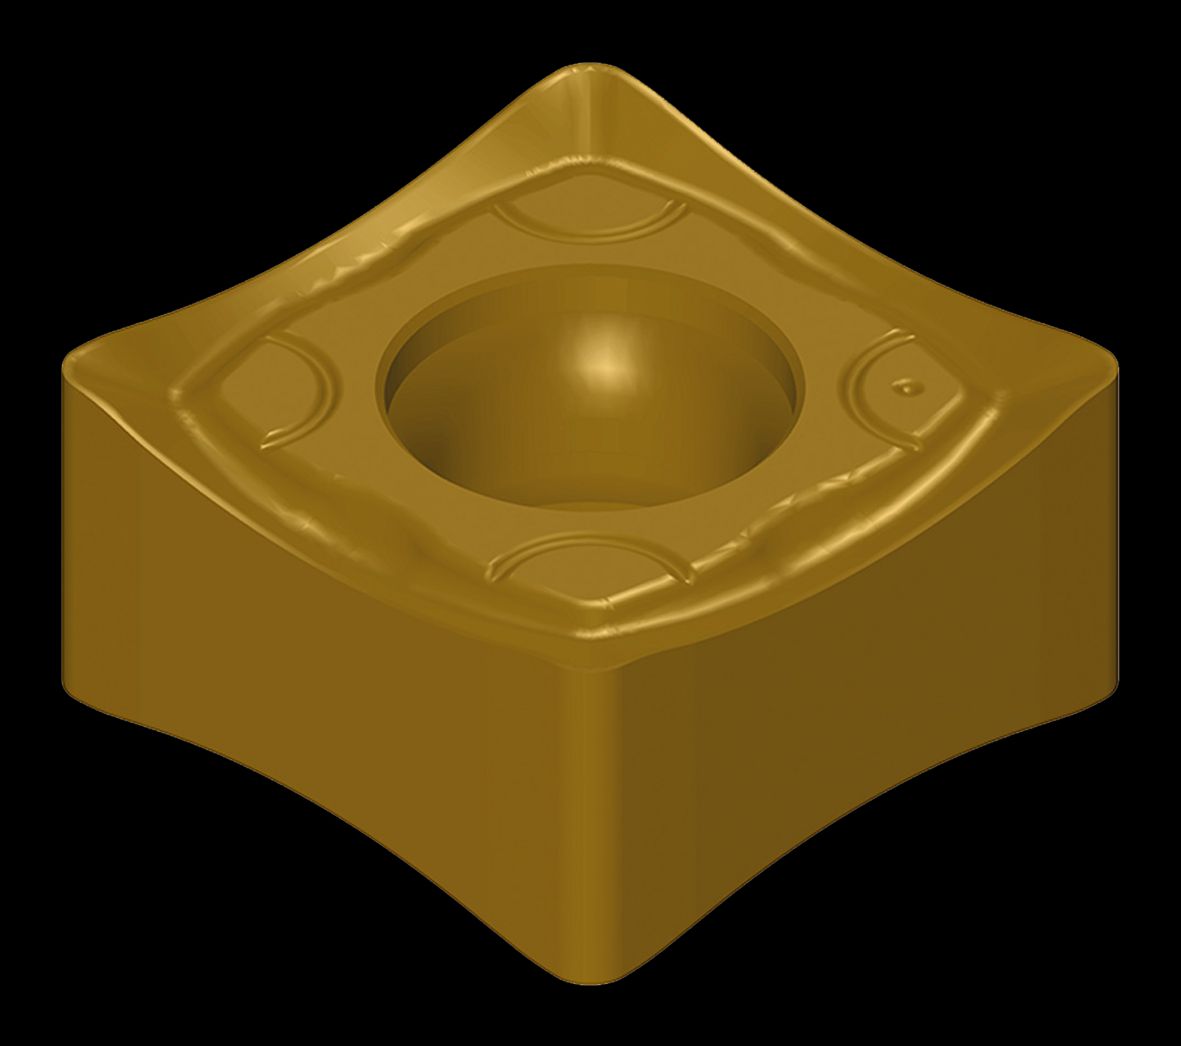

SNMX 120608 SN-MK BCK20M
Product data
chip breaker Description of chip breaker (z.B.: MP= medium application steel , RKH= roughing application cast ironHFC, FMP= Fine and medium application steel,...) | MK |
grade Description of cutting grade (f.e. BCP25M, BCK20M, BCP20T, etc.). | BCK20M |
name of tool system Description of the tool system. | THETAtec 88N |
K1 main K – Cast iron materials, K1 0.6010 (GG-10, GG 10) | 220 - 360 |
K2 main K – Cast iron materials, K2 0.7040 (GGG-40) | 150 - 190 |
K3 main K – Cast iron materials, K3 0.8035 (GTW-35-04, EN-GJMW-350-4) | 170 - 240 |
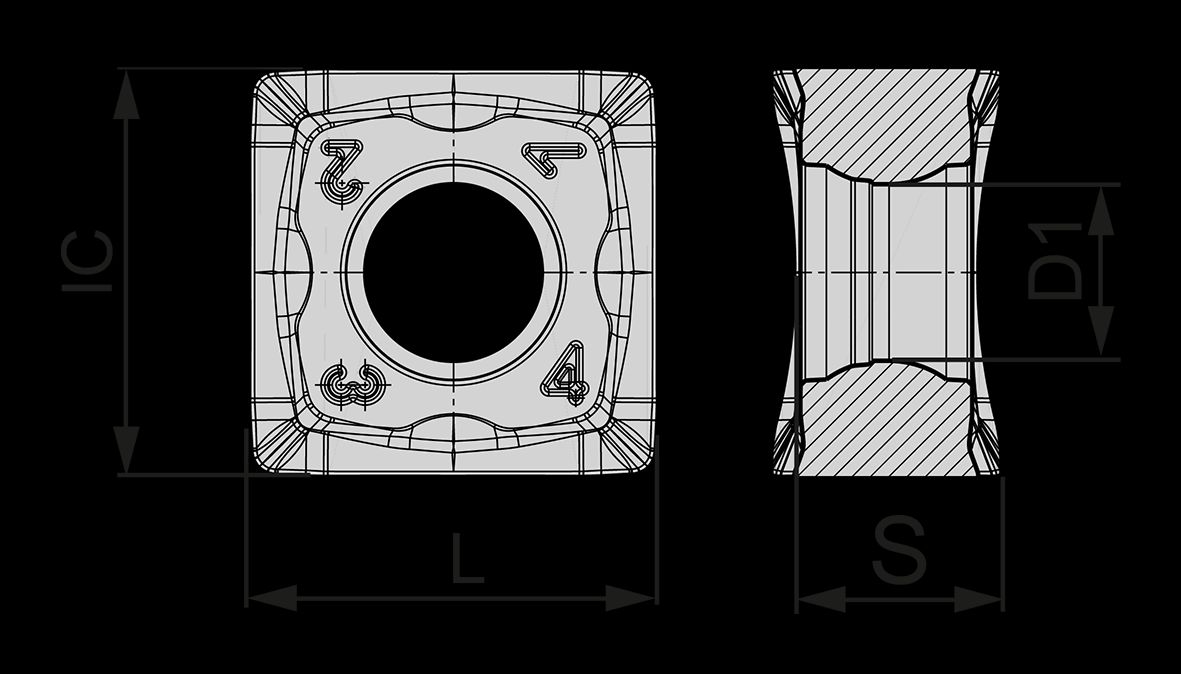
| corner angles [EPSR] | 90 |
| length of cutting edge [L] | 12.7 |
| inner circle [IC] | 12,7 |
| cutting edge height [S] | 5.8 |
| corner radius [RE] | 0.8 |
insert execution r/n/l [IH] AExecution of indexable insert running direction R= Indexable insert right hand cutting L= Indexable insert left hand cutting N= for both cutting directions | N |
| insert height [S1] | 6.35 |
cutting material [GRADE] Description of grade(f.e.BCP25M, BCK20M, BCP20T, etc.). | BCK20M |
coating [COATN] Description of coating. | PVD |
Norm [NSM] Indicates the standard to which the product belongs. | DIN-4000-76 |
H1 secondary H – Hardened materials, hardened cast iron, H1 1.2343 52HRC (X38CrMoV5-1) | 100 - 140 |
H2 secondary H – Hardened materials, hardened cast iron, H2 1.2714 60HRC (55NiCrMoV7) | 80 - 120 |
H4 secondary H – Hardened materials, hardened cast iron, H4 0.9620 52HRC (G-X260NiCr42) | 90 - 130 |
| P1 secondary | 220 - 280 |
P2 secondary P – Steel, P2 1.2312 (40CrMnNiMoS8-6-4) | 190 - 240 |
P3 secondary P – Steel, P3 1.2085 (X33CrS16) | 150 - 190 |
P5 secondary P – Steel, P5 1.1120 (GS-20Mn5) | 140 - 200 |
coating coating type CVD or PVD. | Doppel-Ferrocon |
insert size The size of the plate is specified in millimetres. | SNMX 1206 |
edges/ insert Number of usable cutting edges per indexable insert. | 8 |
insert shape The insert-type describes the shape of the insert. | SNMX |
2D Drawing
Contact
