UP06.010.054 Cx Z4 HBProduct
Pictogramm_DIN.pngProduct
Pictogramm_HB.pngProduct
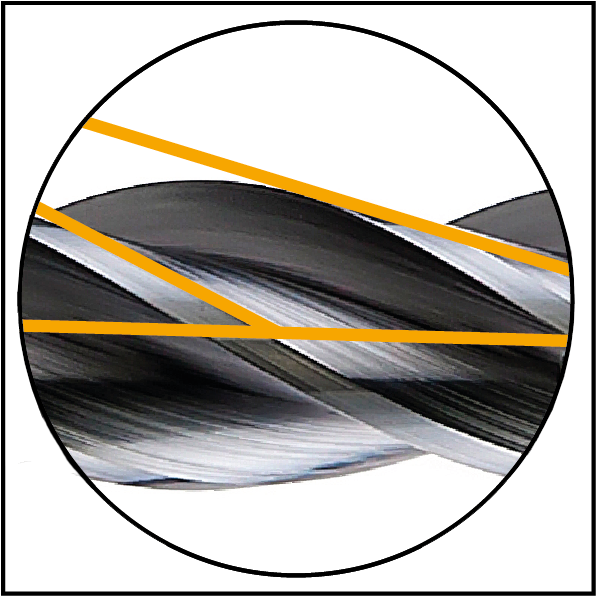
Pictogramm_Ungleiche-Drallwinkel.pngProduct
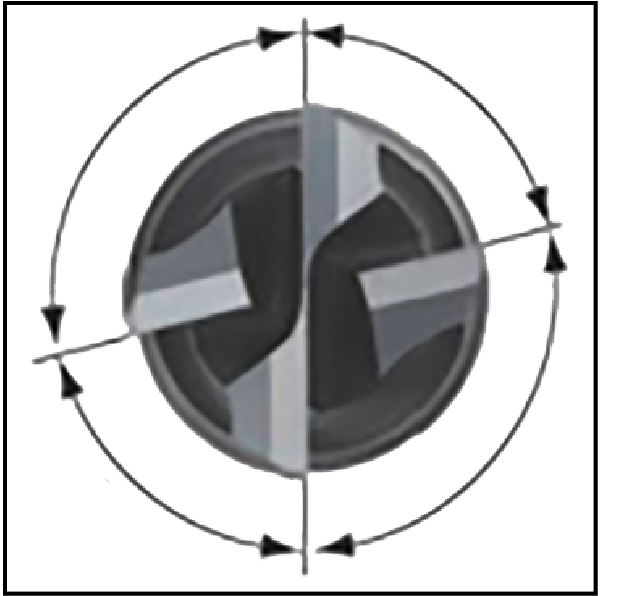
Pictogramm_Ungleichteilung.pngProduct
Pictogramm_Pro.pngProduct
Pictogramm_Cx.pngProduct
Pictogramm_Besaeumen.pngProduct
Pictogramm_Eckfraesen.pngProduct
Pictogramm_Nutfraesen.pngProduct
Ordernumber
5162947
Solid carbide milling general machining
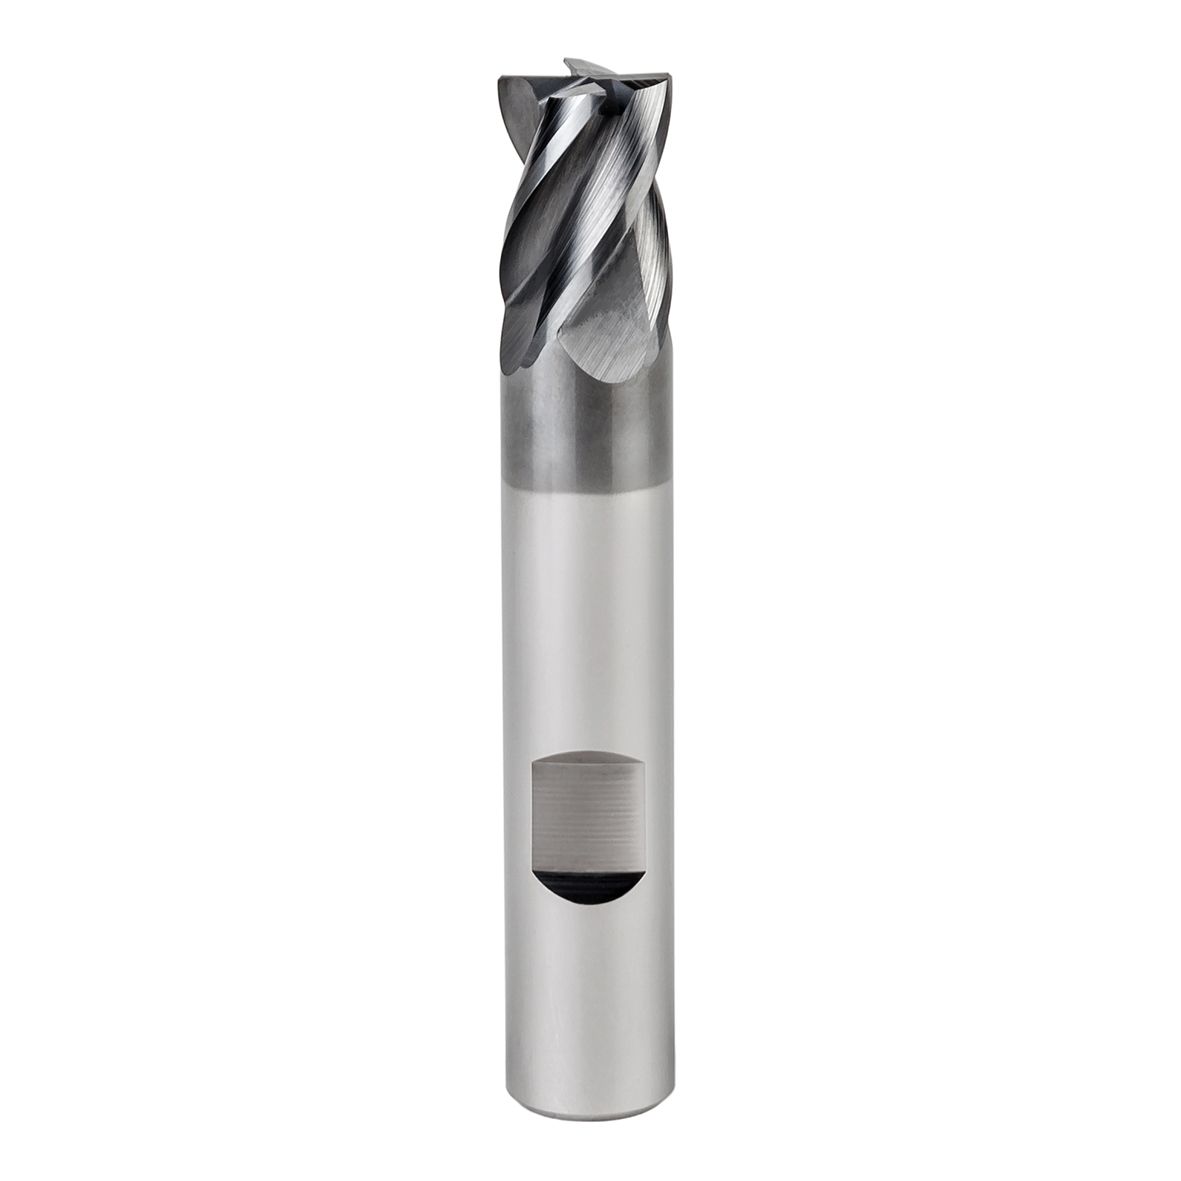
Solid carbide milling tool from the UNItec Pro line in a short execution. Protective chamfer at the cutting edge for more stability and Z4 for more performance and higher cutting rates in common milling in general machining. Very smooth cutting behaviour thanks to special micro-geometry and drag-ground cutting edge. Can be used for all common steel, cast iron and stainless materials.

Product data

grade

Description of cutting grade (f.e. BCP25M, BCK20M, BCP20T, etc.).

VHM PVD
delivery quantiy min

The minimum delivery quantity must be fulfilled for an order.

10
name of tool system

Description of the tool system.

UNItec
P1 main

P – Steel, P1
Material classification:

1.0037 (S25GT)
1.0503 (C45)
1.0718 (11SMnPb30)
1.1158 (C25E)
1.1191 (C45E)
1.1203 (C55E)
1.1274 (C101E, C100S)

180 - 655
P2 main

P – Steel, P2
Material classification:

1.2312 (40CrMnNiMoS8-6-4)
1.2714 (55NiCrMoV7)
1.3505 (100Cr6)
1.6587 (17CrNiMo6, 18CrNiMo7-6)
1.7225 (42CrMo4)
1.7361 (32CrMo12)
1.7715 (14MoV6-3)
1.8523 (39CrMoV13-9)

140 - 595
P3 main

P – Steel, P3
Material classification:

1.2085 (X33CrS16)
1.2343 (X38CrMoV5-1)
1.2379 (X153CrMoV12)
1.2581 (X30WCrV9-3)
1.2601 (X165CrMoV12)
1.3243 (HS6-5-2-5)
1.3343 (HS6-5-2)
1.7701 (51CrMoV4)

110 - 385
P4 main

P – Steel, P4
Material classification:

1.4006 (X12Cr13, X10Cr13)
1.4034 (X46Cr13)
1.4057 (X19CrNi17-2)
1.4510 (X3CrTi17)
1.4542 (X5CrNiCuNb16-4)
1.4747 (X80CrNiSi20)

90 - 265
P5 main

P – Steel, P5
Material classification:

1.1120 (GS-20Mn5)
1.5419 (GS-22Mo4)
1.6571 (GS-34CrNiMo6)
1.6750 (GS-20NiCrMo3-7)
1.7231 (G42CrMo4)
1.7379 (GS-18CrMo9-10)

90 - 400
M1 main

M – Stainless steel, M1
Material classification:

1.4301 (X5CrNi18-10+F3:F21A3F3: F23F3:F24A3F3:F23F3:FF3:F24)
1.4305 (X8CrNiS18-9)
1.4401 (X5CrNiMo17-12-2, X4CrNiMo17-12-2, X5CrNiMo18-10)
1.4404 (X3CrNiMo17-12-2)
1.4541 (X6CrNiTi18-10)
1.4571 (X6CrNiMoTi17-12-2)
1.4841 (X15CrNiSi25-20)
1.4958 (X5NiCrAlTi31-20)

60 - 195
M2 main

M – Stainless steel, M2
Material classification:

1.4362 (X2CrNiN23-4 (Ally 2304))
1.4462 (X2CrNiMoN22-5-3)
1.4501 (X2CrNiMoCuWN25-7-4)
1.4871 (X53CrMnNiN21-9)
1.4310 (X9CrNi18-8, X10CrNi18-8)

55 - 180
K1 main

K – Cast iron materials, K1
Material classification:

0.6010 (GG-10, GG 10)
0.6015 (GG-15, GG 15)
0.6020 (GG-20, GG 20)
0.6025 (GG-25, GG 25)
0.6030 (GG-30, GG 30)
0.6035 (GG-35, GG 35)
0.6040 (GG-40, GG 40)

240 - 715
K2 main

K – Cast iron materials, K2
Material classification:

0.7040 (GGG-40)
0.7050 (GGG-50)
0.7060 (GGG-60)
0.7070 (GGG-70)
5.3400 (EN-GJS-800-10)
5.3403 (EN-GJS-1050-6)
5.3404 (EN-GJS-1200-3)

100 - 655
K3 main

K – Cast iron materials, K3
Material classification:

0.8035 (GTW-35-04, EN-GJMW-350-4)
0.8040 (EN-GJMW-400-5, GTW-40-05)
0.8045 (EN-GJMW-450-7)
0.8135 (EN-GJMB 350-10)
0.8145 (EN-GJMB 450-6, GTS-45-06)
0.8155 (EN-GJMB 550-4, GTS-55-04)
0.8165 (EN-GJMB 650-2, GTS-65-02)
0.8170 (EN-GJMB 700-2, GTS-70-02)

150 - 475
coating [COATN]

Description of coating.

PVD
connection diameter machine [DCONMS]6
shank length [LS]44
cutting direction [HAND]R
tool execution [BMC]H
cutting diamter [DC]6
cutting edge length max. [APMX]10
total length [OAL]54
number of edges usable, circumference [ZEFP]

Number of edges usable, circumference.

4
number of edges usable, face side [ZEFF]

number of edges usable, face side.

4
twist direction [FHH]R

2D Drawing

2D Drawing

Contact

Do you have any questions?
Your contact for Cutting:

Your contact for Cutting:

Boehlerit Service+43 (3862) 300-0[email protected]